






Carcasa de motor mecanizada CNC para vehículos eléctricos: Principales desafíos de fabricación & Soluciones
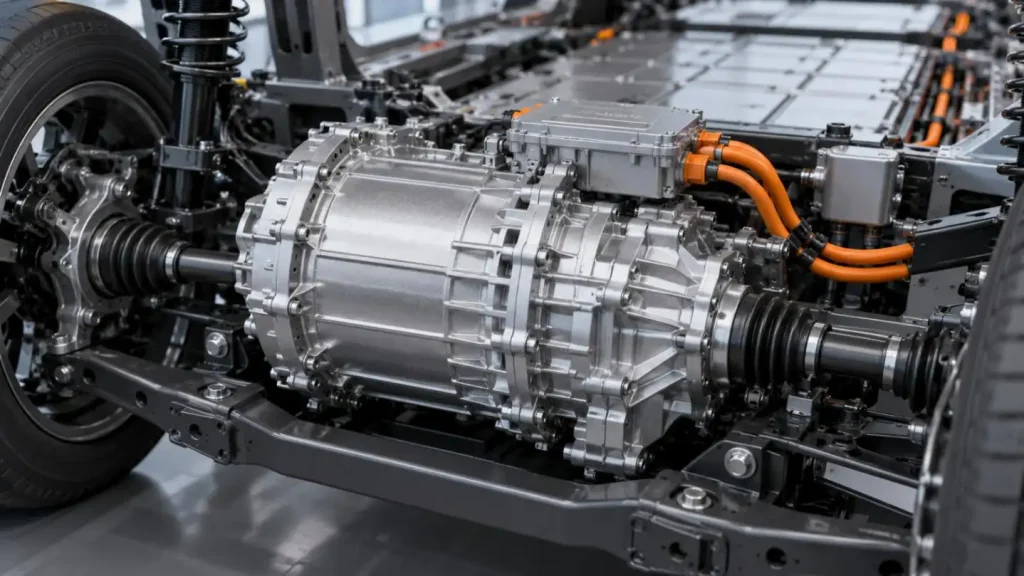
Una carcasa de motor mecanizada CNC es un componente estructural y de precisión, no simplemente un recinto. En una unidad de tracción de un vehículo eléctrico, La carcasa puede localizar el estator, Asientos con soporte, mantener la alineación rotor-estador, proporcionan interfaces de sellado, Transferir cargas estructurales, e integrar funciones de refrigeración.
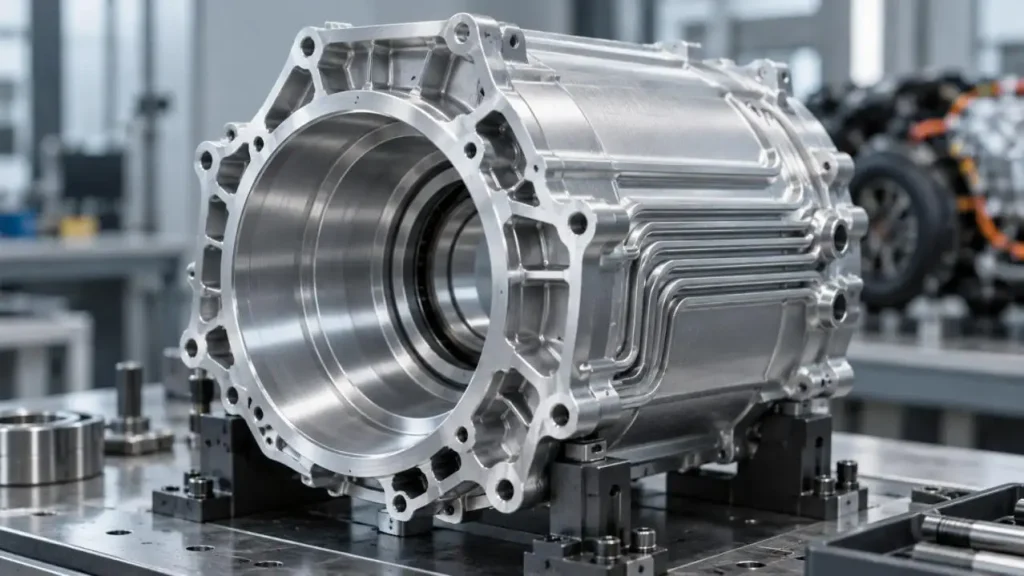
En GD Prototipado, we therefore evaluate a CNC Machined Motor Housing around four connected factors: Control de datos, Estabilidad dimensional, Gestión térmica, y estrategia de inspección. Optimizing only nominal dimensions is rarely enough.
Where Does Motor Housing Machining Become Difficult?
The difficulty comes from combining large material removal with precision features that must remain geometrically related.
| Critical Area | Manufacturing Risk | Engineering Focus |
| Diámetros de rodamientos | Misalignment, Runout | Common datums, finish boring |
| Muros delgados | Distortion after unclamping | Staged machining, fixture control |
| Mounting faces | Flatness error | Stress and thermal management |
| Cooling passages | Tool-access limitations | DFM, Mecanizado multiejes |
| O-ring grooves | Leakage | Anchura, Profundidad, Acabado superficial |
| Multiple-side features | Datum accumulation | 4/5-axis setup reduction |
For a CNC Machined Motor Housing, these characteristics should be considered as one tolerance system rather than independent dimensions.
1. Diámetros de rodamientos: Control Geometry, Not Only Diameter
Bearing-seat accuracy is one of the first areas we review.
A drawing may specify the correct bore diameter while still allowing problems with:
• Cylindricity;
• Circular or total runout;
• Position relative to mounting datums;
• Perpendicularity to reference faces.
Repeated re-clamping can introduce datum-transfer error. Por esta razón, related bores and critical faces should be machined from a common datum system whenever practical.
For a precision CNC Machined Motor Housing, our preferred process logic is:
Rough machining → Dimensional stabilization → Semi-finishing → Critical finishing → CMM verification
Five-axis machining is useful when bearing locations, Puertos laterales, mounting faces, and angled features can be completed with fewer setups. It should not, sin embargo, replace sound datum design.
2. Thin-Wall Distortion Must Be Planned Before Cutting
EV designers naturally want lower mass, but removing material changes the stress balance of aluminum billet.
Typical causes of distortion include:
• Residual stress in raw stock;
• Asymmetric material removal;
• Excessive clamping pressure;
• Cutter deflection;
• Local heat generation;
• Finishing a thin wall before surrounding material is removed.
For thin-wall CNC Machined Motor Housing components, we typically leave controlled finishing stock and avoid taking critical dimensions directly from heavy roughing operations.
Fixture force is equally important. A housing may measure correctly while clamped but move out of tolerance immediately after release.
A representative GD Prototyping 6061-T6 aluminum housing project involved 1.2 mm minimum walls, ±0.02 mm critical-feature tolerance, ±0.05 mm general tolerance, 0.025 mm mating-face flatness, and Ra 1.6 μm pre-anodize finish. The part was produced using five-axis CNC milling with CMM verification.
3. Thermal Control Has Two Different Meanings
During Machining
Aluminum responds quickly to temperature changes. Heavy roughing followed immediately by precision measurement may produce misleading results.
For critical CNC Machined Motor Housing features, process planning may require:
• Controlled coolant delivery;
• Balanced material removal;
• Stable finishing conditions;
• Temperature normalization before final inspection.
• During motor operation
The finished housing may also form part of the EV thermal-management system.
Cooling jackets and channels introduce additional requirements for:
• Cutter or drill access;
• Espesor mínimo de pared;
• Sealing lands;
• O-ring grooves;
• Intersecting passages;
• Plugs and threaded ports;
• Leak-testing access.
A thermally efficient channel that cannot be machined, limpiado, sealed, or inspected consistently is not a production-ready design.
4. Choosing the Appropriate Material and Methods of Manufacture
6061-T6 aluminum is relatively easy to machine compared to other aluminum alloys and, así, is a good choice for prototyping CNC machined motor housings. It also resists corrosion, is anodizing compatible, and has good general availability.
Other alloys can also satisfy functional requirements and do so with greater strength.
Aluminio, as well as other alloys, can be CNC machined to very close tolerances with GD Prototyping. Machining capability of GD Prototyping, 3-, 4-, y máquinas CNC de 5 ejes, with respect to positioning and tolerance, is +/-0.005in (00,13 mm). On a motor housing, tighter tolerances may be possible, but are limited by the wall thickness, material, and the definition of the datum features.
Production volume also changes the process decision:
| Fase de desarrollo | Typical Manufacturing Route |
| Engineering prototype | Billet CNC machining |
| Validación funcional | Mecanizado CNC |
| Producción de bajo volumen | Mecanizado CNC multieje |
| Higher-volume production | Casting/near-net shape + CNC finishing |
CNC machining is therefore particularly useful before tooling is justified or while EV designs are still changing.
5. DFM Decisions That Reduce Risk and Cost
Before releasing a CNC Machined Motor Housing, we recommend reviewing five questions.
Are all tight tolerances functional?
Reserve tight tolerances for bearing seats, locating features, sealing interfaces, and other function-critical geometry.
Can critical features share datums?
A clear datum structure simplifies machining and inspection while reducing tolerance accumulation.
Are internal radii realistic?
Very small internal radii require smaller tools, longer machining time, and potentially greater tool deflection.
Are thin walls supported?
Wall thickness must be evaluated together with wall height, unsupported span, Profundidad de bolsillo, and nearby material removal.
Can every feature be machined and inspected?
Cooling channels, deep threads, ranuras de sellado, and internal bores need both tool access and measurement access.
6. Inspection Should Follow Function
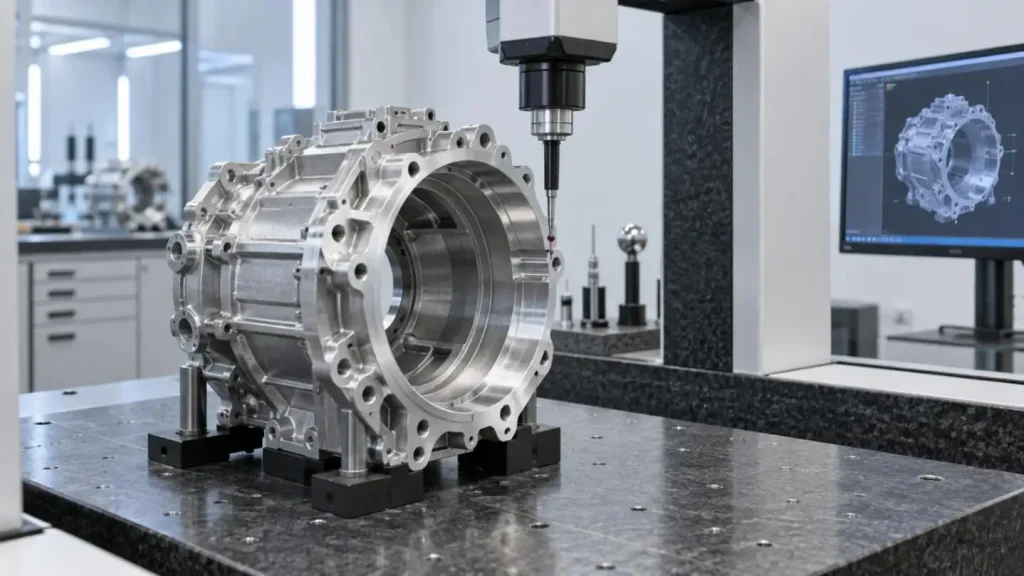
A professional inspection plan for a CNC Machined Motor Housing should not simply measure every dimension equally.
Priority normally goes to:
• Bearing bore size and geometry;
• Datum-to-bore position;
• Mounting-face flatness;
• Sealing surfaces and grooves;
• Threaded-port position;
• Critical wall thickness;
• Rugosidad superficial.
GD Prototyping uses CMM and complementary dimensional inspection for precision housing work. In one automotive aluminum housing project, a 1.4 mm minimum wall, ±0.02 mm critical tolerance, Ra 0.8 μm external finish and Ra 1.6 μm internal finish were specified for a 75-part low-volume build.
From CAD to a Manufacturable Motor Housing
A reliable CNC Machined Motor Housing results from matching design intent with machining reality. Alineación de rodamientos, Estabilidad en la pared, Comportamiento térmico, cooling geometry, Selección de datos, Requisitos de superficie, inspección, and production volume all influence the final manufacturing route.
En GD Prototipado, our role is not only to machine the supplied geometry. For prototype and low-volume aluminum housings, we can review the CAD model and drawing for machining access, Estrategia de tolerancia, Riesgo de pared delgada, Planificación de partidos, and inspection requirements before production begins.
If you are developing a CNC Machined Motor Housing for an EV motor or related powertrain system, you can share the 3D CAD file, Dibujo 2D, material, Cantidad, Acabado superficial, and critical GD&T requirements with GD Prototyping for a practical DFM and manufacturing review.
Discuss your CNC Machined Motor Housing project with GD Prototyping.
Preguntas frecuentes
Q1. What CNC machining capabilities does GD Prototyping offer for motor housings?
El prototipado GD soporta 3 ejes, 4 ejes, 3 2 ejes, and full 5-axis CNC machining, así como torneado CNC. Multi-axis machining is particularly useful for a CNC Machined Motor Housing with bearing bores, Puertos laterales, mounting faces, and complex features that must maintain positional relationships.
P2. ¿Qué aleaciones de aluminio puede hacer una máquina de prototipado GD??
Common aluminum options include:
• 6061
• 7075
• 2024
• Other machinable aluminum alloys
6061-T6 is often suitable for prototype housings because it combines machinability, Resistencia a la corrosión, Rendimiento mecánico, and good finishing characteristics.
P3. ¿Qué tolerancias puede alcanzar el prototipado de GD??
GD Prototyping publishes machining capability of up to ±0.005 mm for suitable high-precision features. Actual tolerance for a complete CNC Machined Motor Housing depends on part size, geometría, Grosor de la pared, Condición del material, Estrategia de datum, y requisitos de inspección.
P4. Can GD Prototyping machine thin-wall aluminum housings?
Sí. In one documented 6061-T6 housing project, GD Prototyping machined a 1.2 mm minimum wall thickness while controlling critical dimensions to ±0.02 mm, general tolerances to ±0.05 mm, and mating-face flatness to 0.025 mm.
P5. How does GD Prototyping control distortion in a CNC Machined Motor Housing?
The machining strategy can include:
• Controlled roughing and finishing
• Balanced material removal
• Dedicated fixture design
• Reduced re-clamping
• Thermal stabilization
• Final dimensional verification
These measures help reduce movement caused by residual stress, machining heat, and clamping forces.
